Delivery time:50-60 days
Payment:30% T/T deposit,70% balance before shipping
Voltage:380V 50HZ 3Phase or based on customer’s need
Warranty:2 years for machinery warranty
Whatsapp: +86 18832797029
e-mail: yuankuoduan@gmail.com
W-Beam Highway Guardrail Roll Forming Machine:
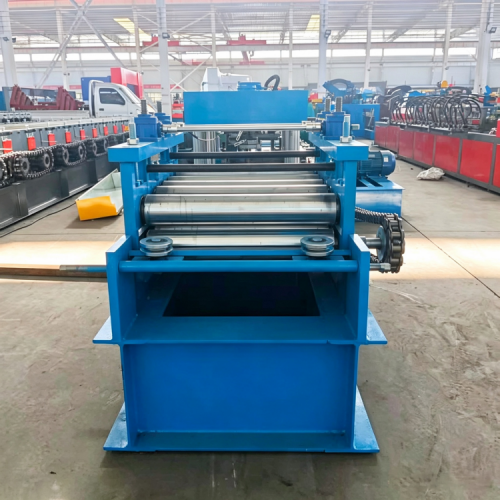
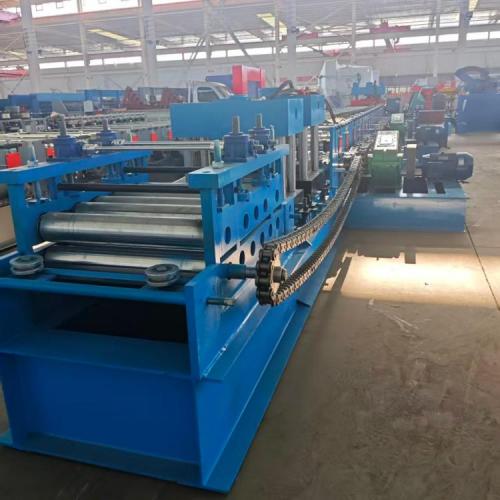
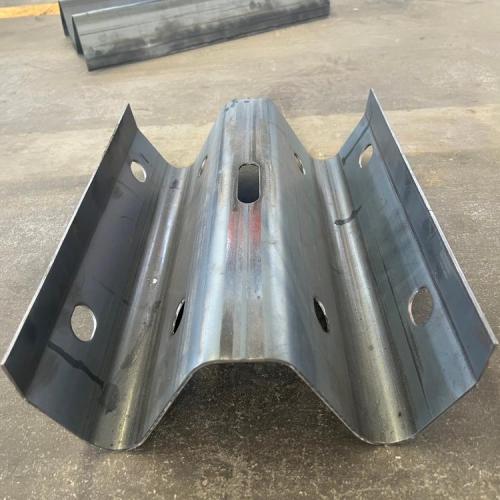
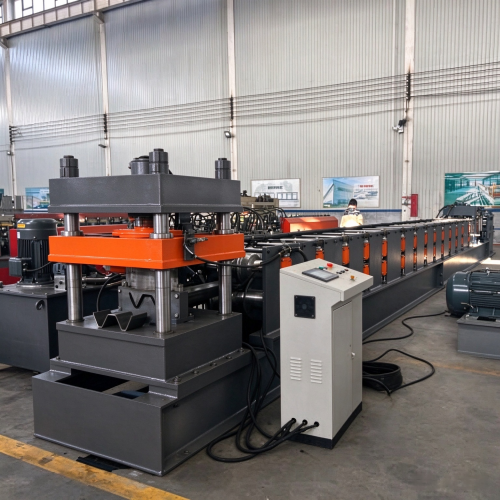
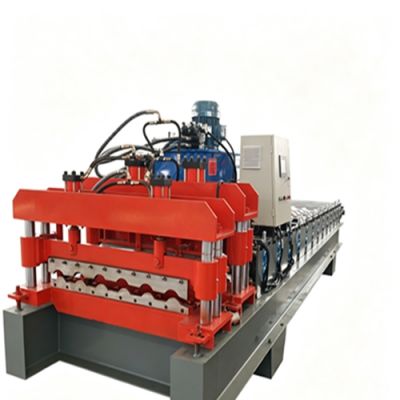
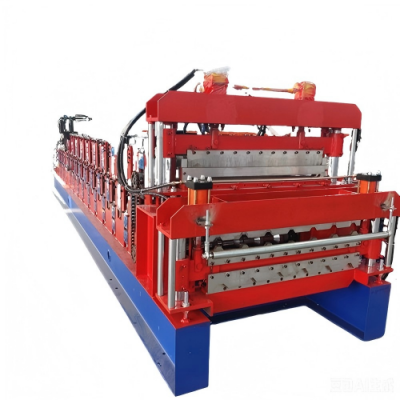
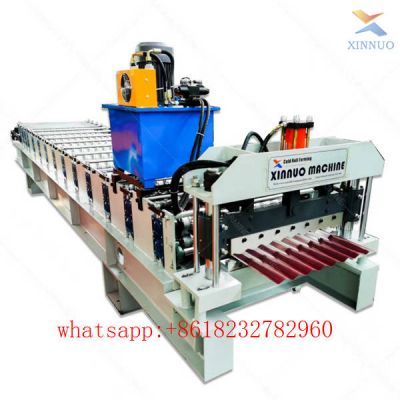
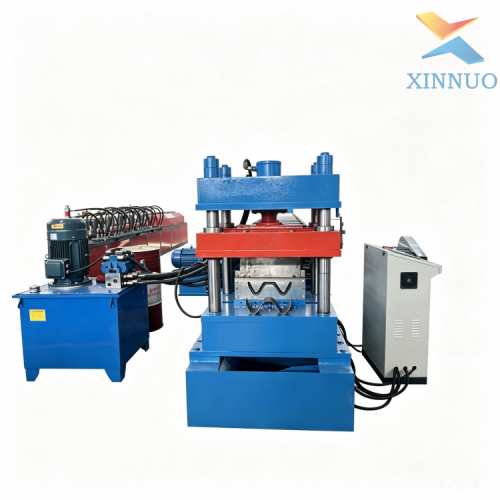
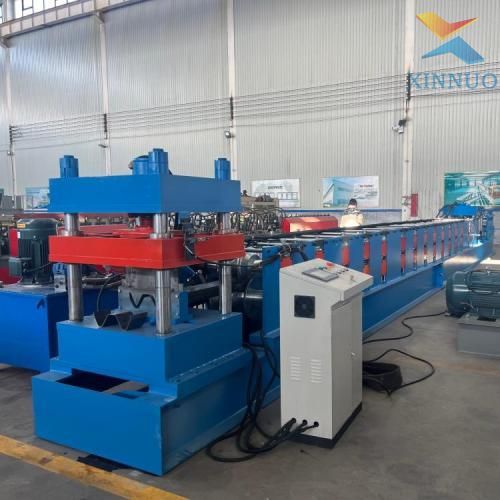
The XINNUO Heavy-Duty W-Beam Highway Guardrail Roll Forming Machine represents an advanced industrial manufacturing solution designed specifically for continuous, high-volume fabrication of standard two-wave crash barrier panels. Widely deployed across national highway projects, expressway expansion corridors, and municipal safety installations, this specialized cold roll forming system converts heavy-gauge galvanized steel coils into high-strength, impact-resistant beam profiles that comply fully with international road safety standards including AASHTO M180, EN 1317, and JT/T 281. Built upon decades of metallurgical expertise and precision engineering, Hebei Xinnuo provides complete turn-key guardrail production lines capable of delivering superior dimensional accuracy, zero surface cracking on zinc coatings, and long-term mechanical reliability under demanding factory duty cycles.
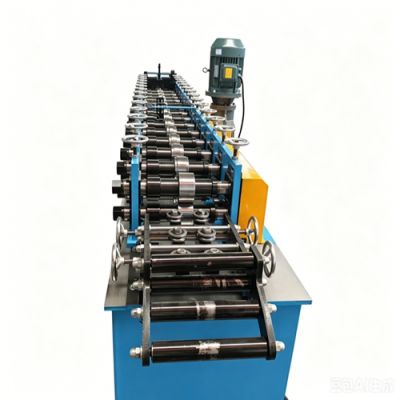
Engineered to withstand the formidable rolling pressures associated with thick steel coil processing (2.5 mm to 3.2 mm, upgradeable to 4.0 mm), the main chassis utilizes an ultra-rigid fabricated H-beam foundation and precision-machined heavy-plate archway stands. Each rolling station is structurally braced to eliminate lateral deflection during multi-stage progressive bending. The machine integrates 16 to 22 forming passes depending on profile specifications. Forming rollers are CNC-lathed from premium GCr15 bearing steel or Cr12 alloy tool steel, followed by vacuum heat treatment and precision hard chrome plating (0.05 mm thickness), yielding a surface hardness of HRC 58–62. Solid 45# forged carbon steel shafts with a diameter of Φ90 mm–Φ100 mm undergo rough turning, quenching, tempering, and final fine grinding to guarantee runout tolerances within ±0.03 mm.
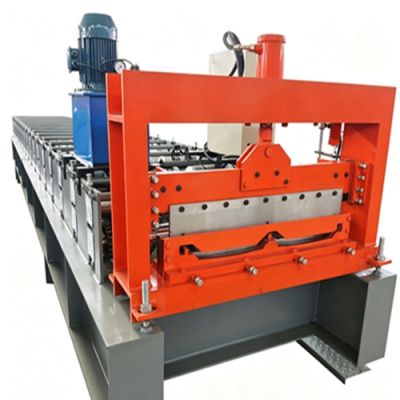
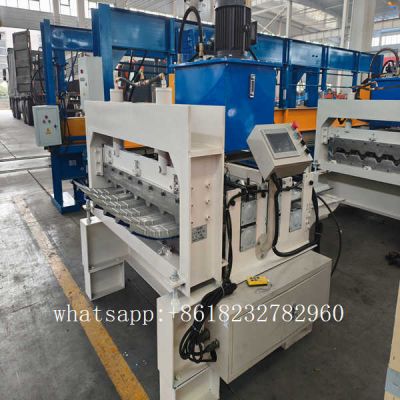
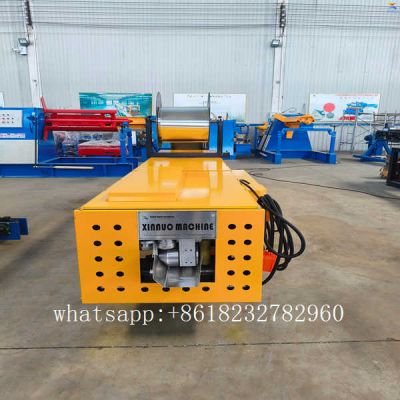
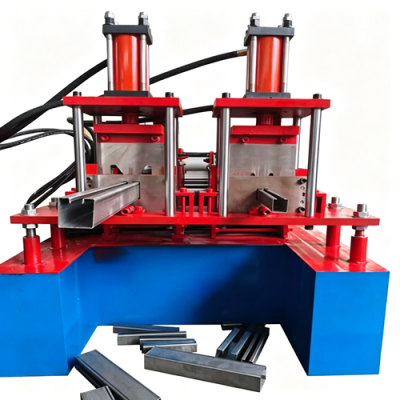
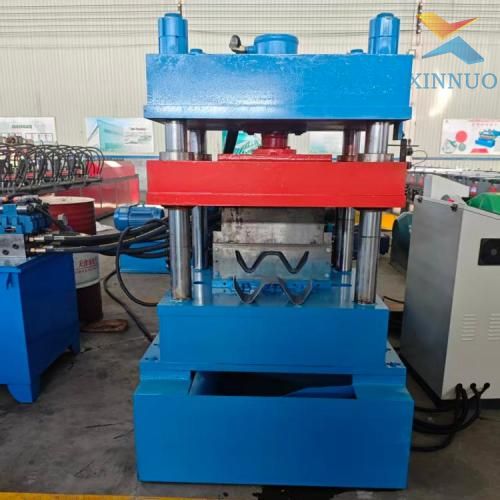
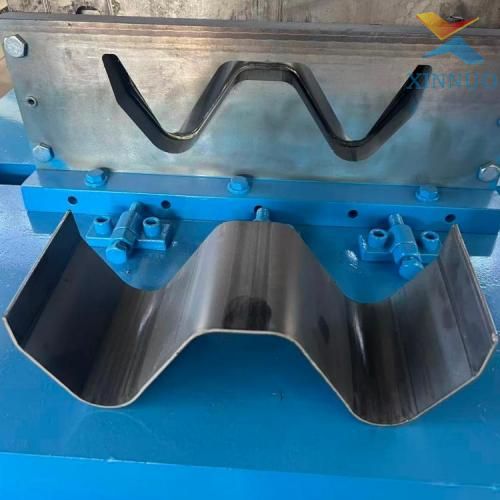
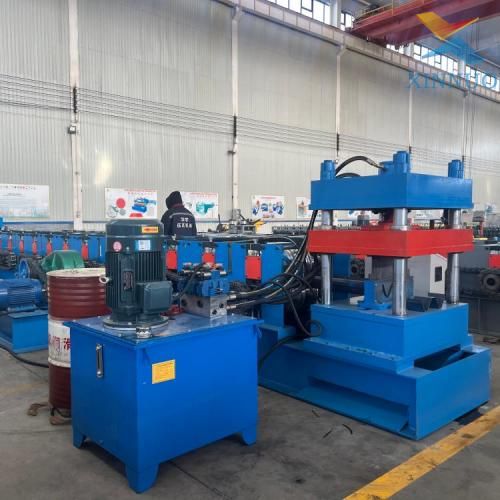
To handle high-yield structural steel, the forming line utilizes a centralized dual-reducer transmission configuration paired with high-tensile 1.5-inch to 2.0-inch heavy-duty drive chains and hardened sprockets, ensuring smooth torque distribution without slippage. The line is equipped with a high-rigidity four-pillar hydraulic post-shearing mechanism. The hydraulic cutting dies, precision-profiled to match the exact W-beam cross section, are machined from vacuum-hardened Cr12MoV tool steel (HRC 60–62). Guided by chrome-plated four-pillar linear tie-rods, the cutter delivers instantaneous, burr-free shearing without edge deformation, maintaining profile symmetry across high-speed continuous cycles. An independent heavy-duty hydraulic power station featuring an integrated cooling and filtration circuit delivers consistent working pressures of 16–20 MPa.
The entire manufacturing workflow is governed by an integrated Mitsubishi or Siemens industrial PLC automation architecture with an intuitive full-color touch-screen HMI. Operators can program single-batch or multi-stage cutting schedules, length offsets, punching hole distances, and piece counts with single-button execution. Dual-channel rotary optical encoders provide continuous closed-loop feedback, achieving finished panel length tolerances within ±1.0 mm and diagonal accuracy within ±1.5 mm. Built-in diagnostic routines, emergency interlocks, and electrical overload protections guarantee continuous operational safety for global factory deployments.
| Parameter Item | Industrial Engineering Standard |
|---|---|
| Applicable Raw Material | Galvanized Steel (GI), Cold-Rolled Carbon Steel (CR), Hot-Dip Galvanized Sheet |
| Material Yield Strength | Q235, Q345, ASTM A36, Grade 50 (Yield Strength: 235–355 MPa) |
| Material Thickness Range | 2.5 mm – 3.2 mm (Customizable up to 4.0 mm) |
| Effective Feeding Width | 482 mm – 488 mm (Standard W-Beam Flat Strip) |
| Finished Profile Dimensions | 310 mm–312 mm (Coverage Width) × 82 mm–85 mm (Wave Depth) |
| Forming Stations | 16 – 22 Progressive Forming Stations |
| Forming Shaft Diameter | Solid Φ90 mm / Φ95 mm / Φ100 mm (High-Grade 45# Forged Steel) |
| Roller Material & Treatment | GCr15 / Cr12 Alloy Steel, Quenched HRC 58–62, Hard Chrome Plated (0.05 mm) |
| Main Driving Motor Power | 22 kW / 30 kW / 37 kW / 45 kW Heavy-Duty Cycloidal Reducer |
| Hydraulic Station Motor Power | 11 kW / 15 kW High-Pressure Dedicated Station (Working Pressure 16–20 MPa) |
| Shearing Mechanism Type | Four-Pillar Guided Hydraulic Profile Cutting (Cr12MoV Die, HRC 60–62) |
| Production Line Speed | 10 – 15 m/min (Standard Line) / 18 – 25 m/min (High-Speed Servo Flying Shear) |
| Electronic Control Architecture | Siemens / Mitsubishi PLC, Touch Screen HMI, Omron/Schneider Components |
| Measurement & Length Tolerance | Dual Optical Encoder Tracking, Precision Within ±1.0 mm per 4320 mm Standard Beam |
| Total Line Footprint | Approx. 18,500 mm × 2,200 mm × 1,650 mm (L × W × H) |
| Total Equipment Weight | Approx. 14,500 kg – 18,000 kg |